
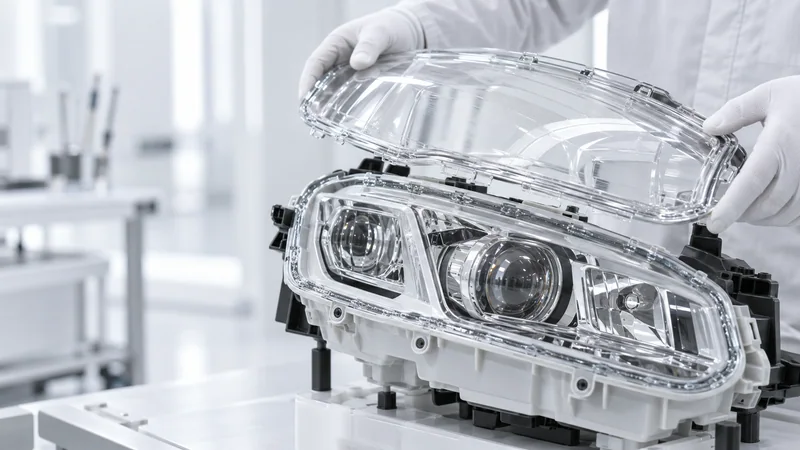
Materials: lens, housing and attachments
List actual grades, treatments and coatings of the proposed bonded parts. Mark proximity to optical surfaces, decorative layers or electronic attachments. Identify the current joining method; discuss adhesive selection only for interfaces whose design calls for adhesive bonding.
- Separate perimeter seams, attachments and locators.
- Record coating boundaries and contact restrictions.
Process: dispensing path and assembly conditions
Use the separately confirmed adhesive and instructions to define cleaning, dispensing path, gap and cure or forming steps. Inspect corners, start/stop points and adhesive distribution after assembly. Specify handling and inspection times instead of importing another application's operating window.
- Record bead continuity and positioning variation.
- Inspect overflow, contamination and neighboring surfaces.
Validation: sealing, appearance and connection strength
Follow customer specifications for connection retention, leakage, environmental cycles and appearance. Optical surface, fogging or condensation requirements need applicable lamp assembly methods, not isolated adhesive results. Where the interface carries structural loads, define that verification separately as well.
- Record leakage, joint failure and appearance.
- Keep structural, sealing and optical acceptance separate.
Project preparation: describe the specific interface
Provide interface drawings, materials, coatings, joint purpose, assembly method and customer tests, including failed samples where available. Confirm adhesive type, current documents and the trial plan separately with RELANET. This page does not claim R-5670 suitability for lighting connections or sealing.
- Identify lamp type, location and stage.
- Include joint inspection and acceptance responsibilities.